
How Does Safety Clamp Work in Lift?

Every day you get in a lift and trust it to stay on its tracks. That trust relies on a device most people never see: the safety clamp. The safety device, known to engineers as the safety brake or safety catch. It is a mechanical brake that grabs the guide rails and stops the car if it is going too fast or if it loses its ropes. Let’s go over how it works, what sets it off, and what keeps it primed. A quick note about the word “lift”. It means a lift for passengers or goods in India. Safety clamps and latches are also used on lifting equipment like hoists, and I cover that meaning toward the end. Quick answer: 5 steps to operate the safety clamp. During normal travel, the clamp’s wedges or rollers are clear of the guide rails with a gap of a few millimetres. The car accelerates too quickly, or the suspension ropes snap. The overspeed governor trips and takes its own rope. The held rope pulls on a linkage that forces wedges or rollers against the rails. That clamp bites, stops the car, and holds it while an electrical switch cuts power to the machine. Here’s why each step occurs. What Is a Safety Clamp in a Lift? A mechanical safety gear called a safety clamp is mounted on the car frame. It straddles the steel guide rails that run the whole height of the shaft. When activated, it locks onto the rails to stop and hold the car. Industry sources refer to the same idea by several names: Safety Equipment Safety Chain Brake Safety catch (old British term) Clamp wedge “Under Indian rules, it is required to be carried. IS 14665 Part 2 has a summary on the overspeed governor and safety gear as mandatory, and IS 14665 Part 4 has a section on lift safety gears and governors. The safety clamp is separate from the ropes and the motor. One guide for home lifts describes the logic nicely: the governor is the sensor and trigger, and the safety gear is the muscle that physically stops the car. The Parts That Make It Work Five main parts come together. Overspeed governor: A sensor, usually at the top of the shaft, that senses speed. It spins with a flyweight mechanism at a speed relative to the car speed. Governor Rope: A rope looping around the governor and tied to the car. It moves with the car Lift rod or linkage: Connects the governor rope to the safety gear on the frame of the car. Wedges, rollers, or cams: hardened blocks located inside the safety gear housing. They hang on the rails. Guide rails: Steel machined rails that the clamp bites against. And also in the chain is an electrical safety switch. When the safety gear works, it cuts off power to the machine. How Does Safety Clamp Work in Lift Systems: Step by Step Step 1: Normal Travel The car runs on the rails, on the guide shoes. The wedges hold back the safety gear that hangs from the frame of the car. A technical source gives a clearance between the wedge and the rail of the order of 2 to 3 mm. No contact during normal riding means the clamp does not wear out. Step 2: Overspeed or Rope Failure Something’s wrong. A rope breaks, the brake gives way, or the car exceeds its limits. The car is beginning to fall too fast. Step 3: The Governor Trips The car goes faster; the governor turns faster. One source says it trips above 115 per cent of the rated speed of the car. Upon tripping, a jaw secures the governor rope to a stationary sheave. Another source calls the signal a mechanical message that runs down to the safety gear linkage. Step 4: The Rope Pulls the Linkage Now the governor rope ceases to move, but the car continues to fall. The downward movement of the car pulls the lift rod through the rope held. This motion either slides the wedges up their sloped surfaces or rolls rollers onto the rail. Step 5: The Wedge Bite and the Car Stops The wedges bear on the machined faces of the rail. The car stops. Friction. Technical sources say the action is self-energising: a harder fall pushes the wedges deeper into the rail. The electrical safety switch cuts off power to the machine at the same time. So the motor cannot continue pulling. The whole sequence is done without electricity, without software, and without the help of the ropes. That’s what independence is for. Instantaneous vs Progressive Safety Gear There are two types of safety gear. It is dependent on the speed and load of the lift. Feature Instantaneous Progressive Stopping action Abrupt, almost immediate Gradual, controlled Deceleration High Kept to a gentle level for passengers Typical use Slow lifts, including many home lifts Faster passenger and goods lifts How it grips Locks wedges or rollers hard into the rail Slides with controlled friction, often using springs The instantaneous type brings the car to a sudden stop, and the progressive type applies braking gradually and reduces the forces on the structure. One source explains that standards classify the type based on rated speed: instantaneous gear for speeds less than about 0.63 m/s and progressive gear for higher speeds. Standards and countries have different limits, so the lift maker must choose the gear that fits the rated speed and rated load. Progressive gear is designed to slow the car down at a rate that passengers can stand, generally characterised as less than 1g. If the shaft has a space such as an office or home below it, the counterweight may also need its own progressive safety gear. What Happens After the Safety Gear Engages The car halts and remains still. What follows is: The car stands still on the rails. The electrical safety device cuts power to the machine. Passengers are advised to remain inside and
Important Role of Material Handling in Logistics
A truck arrives with three drums, forty pallets, and a crated machine. Somebody’s got to unload ’em. Check ’em. Store ’em. Pick ’em. Reload ’em. And not break anything or anyone. And that “somebody” is material handling, influencing almost every facet of a logistics operation. We’ll look at what it covers, where it fits and how to get it right. Quick answer: Material handling is the movement, protection, storage and control of goods within a facility, or between a building and a vehicle. In logistics, it serves six major functions: It handles the movement of goods from receiving to storage to picking to shipping. It safeguards products against damage. It takes strain and injuries off workers. It takes up less space in storage. Accurate inventory control is provided. It helps to keep the labour and handling costs down. Here’s why each one matters. What Is Material Handling in Logistics? Material handling is defined by industry sources as the movement of goods over short distances within a building or between a building and a transport vehicle. It covers the movement, protection, storage and control of materials in warehouses, factories and distribution centres. The job involves packing goods for shipment, loading and unloading vehicles and arranging materials in storage facilities. There are three manners of handling: Manual: Manual lifting, carrying, pushing and stacking of loads. Mechanised Equipment such as hoists, forklifts and conveyors move the load and people control it. Automated: Goods are moved by robots and storage and retrieval systems with little human input. In India, most warehouses and yards are a mix of all three. Where Handling Fits in the Logistics Chain All shipments go through the same steps. Handling is present at each. Receiving: unload the vehicle and inspect the goods. Put-away: The placement of goods in racks, floor stacks, or yards. Storage – Keep your goods safe and make them searchable. PICKING: Collect items for an order. Packing and staging: Prepare order for shipment. Loading: Load the outbound vehicle with goods. Transfer: Transfer loads between docks, yards and vehicles. A weak link at any point delays the rest. A pallet in the receiving bay for six hours causes a backlog of everything that follows it. Material Handling in Logistics by the Numbers India’s logistics sector is big, and its cost is now better understood. The total logistics cost for 2023-24 is 7.97 per cent of GDP and 9.09 per cent of non-services output, a study conducted by the National Council of Applied Economic Research (NCAER) for the Department for Promotion of Industry and Internal Trade (DPIIT) said. Previous estimates of 13 to 14 per cent were based on partial or external data. And the same study takes a hard look at warehousing. It says the average cost is around ?30 per sq ft per month, and manpower is the biggest cost component, accounting for about 30% of warehousing expenses. That last figure is one to be reckoned with. Handling equipment determines how much labour a job requires, and labour is the largest cost in a warehouse. Every time a hoist or trolley takes a lift off a worker’s back, it changes the time and risk.” Seven Roles Material Handling Plays in Logistics 1. It Keeps Goods Moving Smooth handling keeps vehicles turning around quickly and keeps stock flowing between zones. Small delays build up. A slow unload creates a queue of trucks, and a queue creates missed slots and overtime. With the right equipment, a small crew can now unload, position and move loads that previously required a larger crew. 2. It Protects Products From Damage Rough handling damages products. Broken drums, squashed cartons and bent steel cost money. Reduced product damage and waste is one of the major benefits consistently listed in material handling sources. Steady loads due to rated slings, matched equipment and controlled lifting. More control is achieved by crews when slow and steady hoists and smooth trolleys are used to place heavy or awkward items. 3. It Reduces Strain and Injuries Warehouses and docks are messing up people. OSHA’s warehousing guidance identifies improper lifting and overexertion as a primary hazard for back injuries. It offers simple advice: install conveyors, overhead hoists or similar equipment and use powered equipment instead of manual lifts for heavy materials. The NIOSH data adds heft. Musculoskeletal injuries cause about 30 per cent of occupational injuries that resulted in lost time, and material movers have the highest number of overexertion injuries, it says. Lifting, carrying, and moving loads can cause sprains and strains, some of the most common dock and warehouse injuries. 4. It Makes Better Use of Space Good handling makes good use of height and floor space. When equipment can safely lift, position and stack loads, more can be stored per square foot. This is important because rent and space are real costs. Material handling guides note core benefits of better use of space, lower labour costs and less waste. 5. It Makes Loading and Unloading Safer Docks are dangerous and busy. A university guide to loading dock safety lists hazards, including being pinned between lifts, the dock and a trailer; lifting and moving heavy or bulky items; and hazards associated with lifting devices and other moving equipment. Good equipment for the load, clear signals and training will reduce those risks. There is no one loading dock standard in OSHA in the United States. It imposes some rules and general duty requirements to cover dock hazards. See what applies to your own state and country. 6. It Supports Inventory Control “Control” is in the definition. The handling steps determine how quickly the stock is received, located, counted and dispatched. Many handling systems are connected to the warehouse management software that offers real-time data on stock levels, locations and movement. Accurate records in a simple yard are maintained by good staging, well-defined zones and consistent handling. 7. It Keeps Costs Under Control Lower labour needs, fewer damaged goods, fewer injuries, quicker turnaround – all lower cost. The savings
10 Importance of Material Handling Equipment in Food Industry
Plants that provide food move a lot of weight. Sacks of flour, drums of oil, stainless vats, motors, conveyors, and pallets all have to be moved somewhere, and they have to be moved safely and cleanly. The equipment that moves it is often an afterthought to the recipe or the packaging line. That’s an error. Here are 10 reasons why the right handling equipment protects your food, your people, and your budget. Quick Answer: Food plants care about handling equipment because it: Encourages food safety and hygiene Contamination from cut risk Prevents injury to workers Keeps production up Limits damage and waste to products Cold chain protection Makes heavy maintenance safe. Decreases dust and explosion hazard Assists with Audits & Compliance Reduces long-term costs This is why they all matter. What Counts as Material Handling Equipment in a Food Plant? The term covers any equipment that lifts, moves, positions, or holds loads. Forklifts, conveyors, and pallet trucks handle the daily product flow. Lifting and rigging gear handles the heavier, less frequent jobs: setting a mixer motor, swapping a pump, lowering a tank, or loading machinery at the dock. The article is based on the second group: hoists, trolleys, floor cranes, winches, slings, and lifting points. They all apply to the whole category alike. 1. It Supports Hygiene and Food Safety Good design is the basis of clean equipment. The FSSAI hygiene rules in India say that equipment and containers that contact food should be made from good-quality materials such as stainless steel or other non-corrosive materials. They should be easy to clean and keep in good condition. US guidance is even more stringent, with food contact surfaces being non-toxic, non-absorbent, non-reactive, non-corrosive, and cleanable, with smooth polished welds and no recessed fasteners. The same logic should apply to handling gear that works near an open product. Sealed joints and smooth surfaces make it easier for dirt to wash away. An exposed-threaded or chipped-coated trolley is a hygiene problem waiting to happen. 2. It Cuts Contamination Risk When a load is moved, something can fall, drip, or rub off. Good handling equipment keeps these risks small. Food-safety standards require that no paint be applied to any surface that comes in contact with food. A product line should be used sparingly, and food-grade lubricant should be used over the product line. FSSAI guidance states that equipment used for food shall not be used for storage of non-food items, and raw and prepared foods shall be stored in separate equipment that is cleaned before each use. Maintenance personnel working in food areas must observe the same hygienic regulations as production personnel. Overhead hoists and lifting points will safely lift a load and keep it off the ground. This lessens drag, spills and contact with filthy surfaces. 3. It Prevents Worker Injuries People tire of lifting heavy loads by hand. A government guide on manual handling in food manufacturing lists common risks from joint and nerve injuries to chronic pain and lists overhead hoists, pallet lifters and height-adjustable trolleys to reduce them. Wherever possible, the first step is to redesign or automate the task. And the data shows this. NIOSH estimates that musculoskeletal injuries account for some 30 per cent of occupational injuries that result in time away from work. Material movers experience the greatest incidence of overexertion injuries. A US health hazard evaluation at a food plant also found that heavy lifting, twisting, and long reaches are associated with a high rate of strains and recommended redesigning equipment to cut the stress of heavy lifting. A chain hoist or lever hoist places the weight on a rated machine, rather than on a person. 4. It Keeps Production Moving Slow, clumsy handling creates bottlenecks. A pallet is sitting at the dock. Four people are waiting for a mixer part. A line sits idle while a motor is swapped out. Mechanical assist devices help workers lift, push, or pull heavy materials. NIOSH associates them with fewer injuries and greater productivity. A tram allows a hoist to travel along a beam. Electric and manual hoists used to require larger crews, but small crews can do a lot of work. 5. It Reduces Product Damage and Waste Rough handling damages food. India’s Ministry of Food Processing Industries has undertaken studies to measure losses at various stages of harvest and post-harvest, such as handling, storage, transportation, and processing. These are attributed to weak supply chain steps, harvesting, collection, sorting, grading, and weak transport and storage facilities, a government reply in Lok Sabha said. The figures tell why this is important. The NABCONS 2022 study found tomato losses to be above 12 per cent, according to a data analysis site. Losses vary by crop and location, but the pattern is clear. Each additional drop, crush, or delay costs product. Lifting gently and carefully will lessen the odds of dings, spills, and broken packs. Slow hoist speeds and smooth trolleys are useful when you put down heavy, fragile loads. 6. It Protects the Cold Chain Chilled and frozen food has a short window. Every hour a load sits on the dock; it gets warmer. Studies in India indicate that fragmented cold chains and slow transport are responsible for the faster spoilage of tomatoes, fish, and poultry. The same data cited a government assessment that found cold-chain gaps in pack houses, ripening chambers, and refrigerated vehicles. Handling equipment can not solve the whole chain, but it does cut the time loads are out of the cold. It all helps to load smoothly, position quickly, and make fewer stops. 7. It Makes Heavy Maintenance Safer Food plants are driven by machines that need servicing: motors, gearboxes, pumps, screw conveyors and mixers. Many weigh hundreds of kilos. Crews cope without proper lifting equipment. A rated hoist, trolley on a beam, and certified slings put you in control of the job. M.A.Zavery: Elephant manual hoists (C21, H-100, Super 100 and DAG 3t), YA Series lever hoist (pulling/positioning), Trolley Series (plain trolley), Yoke G100
How Multiple Manual Hoists Are Used to Lift Heavy Loads?
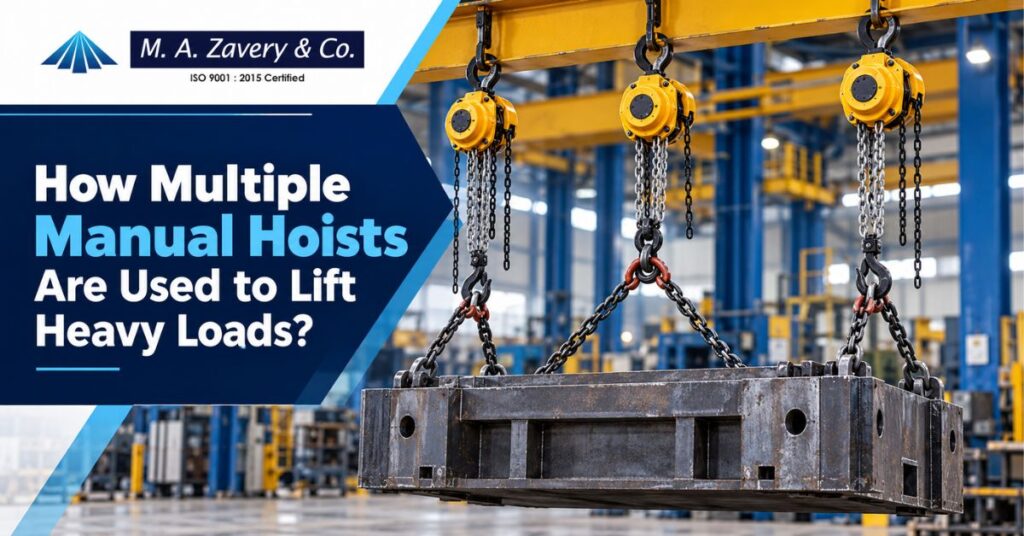
Sometimes one hoist isn’t enough. The load is too long, too awkward, or too heavy for the unit you own. A neat fix would be two or three hand hoists sharing the job. It can work, but it’s one of the easier ways to get hurt if the lift isn’t planned well. This is how crews do it, what can go wrong, and when a single bigger hoist is the better call. Short answer: Yes, more than one hand hoist can lift the same load if the lift is planned and engineered. The basic steps are: Balance the load and locate the centre of gravity. Select lifting points and rated anchors directly over them. “Size each hoist for its share of load plus margin.” Slings and shackles: rig. Rated. Test lift a few centimetres, check level and brakes. Raise in small equal steps with one signalman controlling. Lower it in the same manner and never leave the load suspended. Every step counts. Why Use More Than One Hoist? If one hoist can’t do the job well, crews reach for two or more hoists. Typical reasons are: Heavy loads. Beams, pipes, tanks, and fabricated frames must be supported at two or more points to remain level. Limited equipment. You have two 3-tonne units, not one 6-tonne unit. Close Quarters. Two lifting points prevent long loads from swinging around. Placement of levels. Independent hand chains allow one end to be raised or lowered. Crane operators refer to this as tandem lifting. One industry guide says that splitting the load between lifting units reduces the risk of overloading any one of them and gives better control over the position of the load. The same reasoning applies to hoists. The same guide also warns that an error in estimating the centre of gravity can lead to one unit carrying more than it is supposed to. The Honest Caveat: Why Safety Documents Discourage It Read this part before you rig anything. Multi-hoist lifts are discouraged in many hoist safety documents. Lifting a load using two chain blocks is not recommended, says one university safe-work procedure. The manual says if the job can’t be avoided, it says to hoist with extreme care and keep the load balanced. It’s an easy concern. Hand chain hoists do not include a means of load sharing. Each operator tugs at their own speed. If one end is up faster, the other hoist takes more weight and can overload. One safety article on tandem lifts says that when coordination breaks down, loads can slide out from under the hoists, and the worst case is a broken chain and a dropped load. So, as a last resort, use these lifts. Use if there is a hoist of the right size. If not, plan the lift in writing, and follow these steps: Manual Hoists to Lift Heavy Loads: Common Setups Setup 1: One Hoist With a Lifting Beam or Spreader This is the safer choice, so start here. The anchor has one hoist on it for lifting a lifting beam or spreader beam. The beam distributes the load over a number of pick points. A lifting beam is typically fitted with a lifting eye at the top and lower eyes below the beam. A spreader beam is a strut loaded in compression. Often used with a two-leg sling. Each is designed for specific loading, so use it the way the maker intended. Setup 2: Two Hoists, Two Anchor Points Two hoists are suspended from two different anchors, one above each pick point. This is suitable for a long load which is balanced between the points. Each hoist pulls straight up, which is important because chain blocks are designed for vertical lifting and should not be used for pulling at an angle. Setup 3: A Twin-Hoist Lifting Beam Some lifting beams are made for two hoists. One example on the market states the beam only works when both hoist lines are within 5 degrees of vertical. Use any beam you want, but watch the limits and keep the lines plumb. Setup 4: A Chain Fall for Fine Levelling For adjustment when a load is off balance, engineers sometimes install a hand chain hoist (chain fall) on a lifting beam. This layout is described exactly in one engineering paper. The adjustment hoist trims the level; the main lift does the job. Setup 5: Hoists on Trolleys The load can also be moved by two hoists on trolleys along a beam. Line up the trolleys; keep the wheels moving together. M.A.Zavery offers a plain trolley of the Trolley Series (washer type) for hand-operated hoists. Plan the Lift: Weight, Centre of Gravity, and Load Share The lift works if planning says so. Do these 4 things first. 1. Find the Total Weight Include rigging, shackles, lifting beam, and load. Rigger standards tell crews to look at the load in terms of size, material, wet or dry, centre of gravity, added components, and the weight of rigging hardware. Don’t guess. 2. Find the Centre of Gravity The point where the load is balanced is called the centre of gravity (CoG). A wrong CoG gives too much weight to one hoist. Mark it on the load before rigging. 3. Work Out Each Hoist’s Share Two pick points: the hoist closer to the CoG carries more. Use this rule. Share on hoist A = Total weight × (distance from CoG to B) ÷ (distance between A and B) Here is a worked example: Item Value Load weight 4,000 kg Rigging weight 150 kg Total 4,150 kg Distance between pick points 6 m CoG distance from A/B 2 m / 4 m Share on hoist A 4,150 × 4 ÷ 6 = 2,767 kg Share on hoist B. 4,150 × 2 ÷ 6 = 1,383 kg Hoist A carries twice as much as hoist B, yet the load looks symmetrical on paper. 4. Pick Hoist Ratings With Margin Each hoist must beat its share plus margin. A 3-tonne unit like
Difference Between Chain Hoist and Chain Block
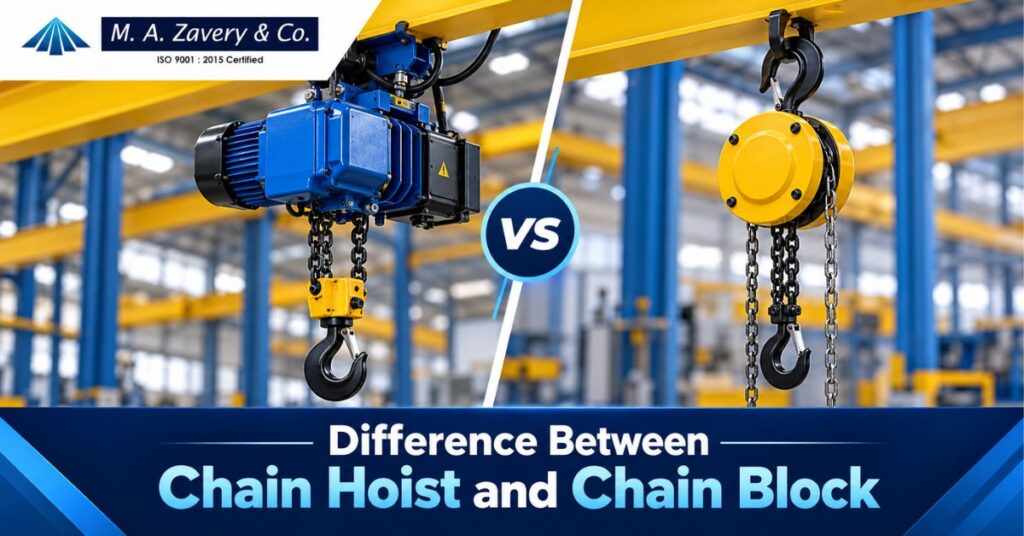
Ask five people on a shop floor, and you might get five answers. “A chain block and a chain hoist,” it is said, “are the same machine. And one says he is manual and one is electric. A third says it’s the type of lever, too. They are all partly right. Let’s break it down so you don’t have to make a second phone call for the right gear. Quick response: A chain block is a hand-operated hoist. It has a hand chain to lift or lower a load. Chain hoist is the larger family. This includes hand chain hoists (chain blocks), lever hoists, electric chain hoists, and pneumatic chain hoists. So all chain blocks are chain hoists, but not all chain hoists are chain blocks. This is why the names overlap and how to choose. What Is a Chain Block? A chain block is a manual hoist for vertical lifting of loads. The machine is suspended from a fixed point, e.g., a beam clamp or trolley. One side has a hand chain, and the other has a load chain running through the body to a bottom hook. That’s how it works. You pull the hand chain down. This causes the gears inside the unit to turn, which then moves the load chain to lift or lower the load. One retailer describes the setup as a static top hook for suspension and a load hook at the bottom, moved by pulling the hand chain. Another source describes the interior as a combination of geared pulleys fitted with a chain. Capacity varies by model. One industry source cites typical hand chain hoist ratings from a quarter tonne to 50 tonnes, although most workshop units are well below that top figure. Each approved unit has a rated load, and the maximum permitted shall never be exceeded. Other Names for a Chain Block Not always the same. Same tool name. Industry sources say that a hand chain hoist is also sometimes called a chain block or a chain fall. You may also like these terms: Chain hoist manuals Hand chain hoist Chain Block Pulley Block and tackle (some retailers loosely call it) Columbus McKinnon, a leading hoist maker, uses ‘chain fall’ for the hand-operated type, and its experts say you can use one anywhere you would use an electric hoist, but without the need for power. That makes it a good choice for remote sites and places with intermittent power. What Is a Chain Hoist? The general term is a chain hoist. Any hoist that lifts with a load chain will do. This family comprises: Hand chain hoists (chain blocks): operated by means of a hand chain Lever hoists: operated by a ratchet handle Electric Chain Hoists, Motor Driven, Pendant Control Air chain hoists: driven by compressed air One supplier says the difference between a hand chain hoist and an electric version comes down to how you operate it: Human effort for one, an electrical connection for the other. That’s the simplest split in the category. When people say “chain hoist”, they often mean the electric type and leave out a qualifier. Always ask what kind they mean before you quote or order. Chain Hoist vs Chain Block: Side-by-Side Comparison Here is how the terms line up in daily use. Feature Chain Block Chain Hoist (broad term) Meaning Hand-operated hoist Any hoist that uses a load chain Power source Your muscle, via the hand chain Hand, lever, electric motor, or air Lift direction Vertical only Depends on type Speed Slow, steady Fast with electric or air Power needed None None for manual, yes for electric and air Typical use Workshops, maintenance, field repairs All of those plus production lines Common confusion Often called a chain fall or manual hoist Often means electric when used alone Why the Names Get Mixed Up A lot of the confusion is explained by regional custom. “Chain block” is common in India, the UK, and Australia. In the US, “chain hoist” is more common. The term “chain hoist” is used everywhere, sometimes for manual units, sometimes for electric ones. Product listings also get mixed in. Here is how the labels change on the M.A.Zavery website. It lists the Elephant H-100 Series as a chain block, the Elephant C21 Series and Super 100 as manual hoists, and the Beta Series as an electric chain hoist. Same family category. 3 labels. If you are unsure, read the product description, not just the title. Chain Block vs Lever Hoist: Another Common Mix-Up People also interchange “chain block” and “lever hoist”. They look the same, but they work differently. An overhead hoist is a chain block which lifts vertically. You pull the hand chain, and it never needs a lever. One UK supplier calls it the perfect answer for repetitive vertical lifting from a fixed overhead point. A lever hoist has a short handle you crank up and down to engage a ratchet and pawl. This design allows it to lift, pull, and tension loads at different angles. The lever block operates by turning the handle. This moves the load a set distance per stroke. Lever hoist working load limits range from 250 kg to 9 tonnes according to supplier guides. A lever hoist is also suitable for lashing and tightening jobs. Here’s a fast guide: Chain block: Lifting a machine vertically off a beam Lever hoist pulling together steel beams Chain block for daily lifting at one post Lever hoist: Tightening a rope or chain Lever hoist: tight spaces where a hand chain has no room Hand chain hoists must be used for vertical lifting only. Use a lever hoist for angled pulls. As an example, the Elephant YA Series lever hoist is listed on the M.A.Zavery site. The two types have different ASME standards too. ASME B30.16 covers hand chain-operated chain hoists and electric and air hoists, and lever hoists have their own volume, B30.21. Chain Block vs Electric Chain Hoist This is the comparison that matters when you
Types of Products Offered by Elephant Brand Hoists

If you have ever spent time in India near a workshop, warehouse, or fabrication yard, you may have heard the name Elephant. It’s a brand that you keep seeing on shop floors because the equipment can stand up to daily use. But “Elephant hoists” are not just one product. A full line-up, covering hand lifting, lever operation, and electric power, all built for a different kind of job. Learn about the complete line of Elephant brand hoists, what each series is designed to do, and how to determine which one is right for your application. Let us take it by series. A Quick Background on the Elephant Brand Elephant is a Japanese manufacturer of lifting equipment known in the industry for its very close attention to build tolerances and durable construction. The company has established a reputation for chain blocks, lever hoists and electric chain hoists that have retained their rated capacity after many years of repeated use, even in rough industrial environments such as foundries, steel yards and construction sites. M.A. Zavery & Co. has been supplying genuine elephant hoists in India since 1983, acquiring stock through authorised channels and backing every purchase with technical guidance regarding capacity and configuration. That long track record counts, because counterfeit or grey-market hoists often skip the load chain grading and braking systems that make the real deal safe to use. Manual Chain Hoists: C21 Series and H100 Series Manual chain hoists are often the first choice for most lifting jobs where power is not available or loads do not need to be lifted frequently. You pull on a hand chain, and the hoist lifts or lowers the load through a gear-reduced mechanism. The C21 Series is a compact hand-operated chain block suitable for maintenance work, workshop lifting and general light to medium industrial use. The hoist has a galvanised load chain, compact housing and a mechanical brake system that locks the load in place at any height when you stop pulling. These lightweight hoists are easy to move between job sites or around a shop floor because of their capacity. The H100 Series is the benchmark for build quality for more demanding, more frequent lifts. Features bearing-supported shafts for low hand-chain pull effort at full rated load and a double brake pawl system for additional holding security. Both ranges have safety latches on the hooks, and the load hook should fail under overload, not snap, so that operators have a visible warning sign before a failure point is reached. The C21 and H100 hoists also come with either plain or geared trolleys if you want to move the load horizontally along a beam and not just vertically. Lever Hoists: YA Series and Y2 Series A lever hoist operates in a different way to a chain block. Instead of pulling a hand chain through a loop, you move a ratchet lever back and forth. This makes them perfect for angled pulls, horizontal pulling, or tensioning work where a chain block’s straight vertical pull isn’t going to do the job. Elephant’s standard lever hoist line, the YA Series, is built for general rigging, tensioning, and positioning applications in construction, pipeline work, and machine installation. It has single-action free spooling, which allows you to quickly pull the slack chain through before engaging the lever mechanism, saving time during setup. The Y2 Series (along with the closely related Y3 Series) completes the lever hoist range with additional capacity options, providing a wider choice to meet varying load and application needs. Typically, lever hoists in this range have a reinforced load chain and a multiple safety factor in the chain, hooks, and braking parts. That is why they stand up to the kind of side load and repeated tensioning that a straight chain block is not designed for. Electric Chain Hoists: Alpha, Beta, SA, FA/FB, and DA/DB Series When your lifting volume is increasing, or the loads are heavy enough to slow production with manual operation, it’s time for electric chain hoists. The Elephant electric range includes single-phase and three-phase power, with options for variable speed or constant speed depending on the series. Alpha Series: Electric hoist with hook suspension, variable and constant speed designs, suitable for general manufacturing and assembly line lifting. Beta Series: Like the Alpha Series in style, but offering single-phase electric operation for facilities needing dependable repeat lifting cycles without the benefit of three-phase power infrastructure. SA Series Hoists for more demanding electric lifting. Available in plain, geared, or electric trolley configurations to meet your load’s travel needs. FA/FB Series: A three-phase electric hoist line for continuous duty applications in manufacturing plants and heavier warehousing operations. DA/DB Series – The higher capacity end of the electric range, designed for heavy-duty lifting where load volume and cycle frequency are high. Any of these electric series may be coupled with plain, geared, or electric trolleys. They are equipped with a hook-suspension that allows an easy installation on an existing beam. If your shop has long shifts with the same load pattern repeated dozens of times a day, the labour savings of an electric hoist will generally pay for the equipment in a reasonable time. Trolleys: Plain, Geared, and Electric A hoist can lift a load up and down, but it cannot move that load side to side by itself. That’s where a tram comes in. The elephant provides a full range of trolleys in both washer and standard type builds, designed to fit directly with the manual, lever and electric hoist series above. A simple trolley has no gears and is pushed by hand. They work well for light loads where only occasional horizontal movement is needed. Geared trolleys use a hand chain and reduction gears to give the operator more control and less physical effort when moving heavier loads or positioning them accurately. Electric trolleys are motor-driven and compatible with the electric hoist series and are ideal for high-frequency lifting, long beam runs, or heavy tonnage that would slow the job down with
How Much Weight Can Elephant Lifting Equipment Lift?
If you have worked with hoists on a factory floor, construction site, or shipyard, you are probably familiar with the Elephant name. It is one of the better-known names in the chain hoist business, appearing on manual hand chain hoists, electric hoists, and trolleys in dozens of industries. But the question most buyers ask before they order is simple: how much weight can elephant lifting equipment lift? The short answer is dependent on the model. Elephant lifting equipment ranges from small hand chain hoists rated at a few hundred kilograms to large industrial hoists rated well past 30 tonnes. This guide breaks down the actual capacity ranges by product type, explains what decides those numbers, and covers how to pick the right one for your job. Let’s take them one by one. What Is Elephant Lifting Equipment? Elephant is a brand of hoists and rigging, including manual chain hoists, electric chain hoists, air (pneumatic) hoists, lever hoists, and the trolleys and beam clamps that run on a rail to carry them. It covers everything from light manual lifting in a small workshop to heavy-duty electric hoisting in a shipyard or steel plant. Elephant’s range includes the C-21 manual chain hoist, the Super 100 series, three-phase and single-phase electric hoist ranges, and matching trolley systems. How Much Weight Can Elephant Lifting Equipment Lift? Capacity is entirely dependent on which product line you select. Based on published manufacturer and distributor specifications, here is the general range across the main categories. Hand Chain Hoists Any line of Elephant products includes the widest range of manual hand chain hoists. (Source: “Hoists, Comealongs, Winches, Beam Crawls”, Elephant Lifting Products, https://elephantlifting.com/) A typical C-21 hand chain hoist starts at about 1 tonne and goes up to 5 tonnes for common workshop and construction applications. Heavy-duty versions of the hand chain hoist range goes much further, with high-capacity models rated between 16 and 50 tonnes for large industrial lifts (Source: “Elephant High Capacity Hand Chain Hoist, 16 Tonne to 50 Tonne”, Ergonomic Partners, https://www.ergonomicpartners.com/high-capacity-hand-chain-hoists). The full hand chain hoist catalogue includes capacities from 1.6 tonnes to 50 tonnes and will meet almost all manual lifting jobs on a site (Source: “Elephant Hoists, Elephant Lifting Systems”, Chainhoist.com, https://chainhoist.com/brands/elephant/). Electric Chain Hoists Electric hoists give up a little of that top-end capacity for speed and less physical strain on the operator. The Elephant DA-3 is a common model rated at 3 tonnes with lift heights of 10, 15, or 20 feet and powered by a single-speed 230V or 460V three-phase motor (Source: “Elephant DA-3 Electric Chain Hoists For Sale”, Hof Equipment Co, https://hofequipment.com/elephant-da-3-electric-chain-hoists-p2436.html). The standard capacities of the broader electric hoist range typically vary from a quarter of a tonne to 5 tonnes for everyday industrial use (Source: “Elephant Hoists, Elephant Lifting Systems”, Chainhoist.com). Large-capacity electric chain hoist models push that range up significantly for heavier jobs, with some series rated from 100 kilograms all the way up to 30 tonnes, and select large-capacity units designed to carry loads up to 30 tonnes all on their own (Source: “Large Capacity Electric Chain Hoists, 10t to 50 Tonne Capacity”, Elephant Lifting, https://elephantlifting.com/product/electric-chain-hoists/large-capacity-electric-chain-hoist/; “Hoists, Comealongs, Winches, Beam Crawls”, Elephant Lifting Products). Air (Pneumatic) Chain Hoists Air hoists are faster than manual hoists but slower than electric hoists and are suitable for hazardous areas where sparking from electrical equipment may be a problem. Standard catalogue (Source: “Elephant Hoists, Elephant Lifting Systems”, Chainhoist.com): Elephant hoists are available from a quarter tonne to 10 tonnes. This makes air hoists a good choice for petrochemical plants, paint booths, and other environments where combustible dust or vapour rules out electric motors in the vicinity. Trolleys and Support Equipment Hoists rarely work in isolation. Push, geared and electric trolleys carry the hoist along an I-beam or monorail, and their own rated capacity has to equal or exceed the hoist mounted on them. Beam clamps and plate lifters round out the range, allowing the same hoist to attach to different beam widths or grab flat steel plate directly. None of these provide any additional lifting capacity above the rating of the hoist attached to them. The whole system, the hoist, trolley, and rigging, is only as strong as its weakest rated component. What Decides the Lifting Capacity of a Hoist? The maximum weight any hoist, elephant or otherwise, can safely lift is limited by a few design factors. Gear ratio and chain type. The mechanical limit on rated capacity is determined by the grade of the load chain (usually Grade 105 galvanised chain on Elephant models) and the reduction gearing inside a manual hoist. Motor power: For electric hoists, motor output, lift speed, and top rated capacity are all connected. Hook and frame strength. The steel frame, hooks, and load sheave all have to be strong enough to match the chain rating; otherwise they become the actual weak point, not the chain. Class duty. Hoists intended for continuous or frequent lifting (higher duty ratings) often have different practical limits than a hoist intended for occasional, light-duty use, even at the same nominal capacity. Lift height and reeving: Longer lift heights and multi-fall reeving (where the chain runs through extra sheaves) change the load distribution across the chain, and this is accounted for when calculating the rated capacity for that config. Safety Margins and Load Testing Standards Rated capacity on the nameplate is never a number to strive for. Reputable chain hoist manufacturers build in a safety margin and test each unit well beyond its rated load before it ships. For instance, Elephant electric chain hoists are made to conform to ASME B30.16, the American standard for overhead hoists, and each unit is load tested to 125 per cent of its rated capacity before leaving the factory (Source: “Elephant DA-3 Electric Chain Hoists For Sale”, Hof Equipment Co). That margin is there to allow for shock loading, wear and tear over time, and small variations in how a load is rigged, not to allow operators to exceed the
Elephant Hoists for Manufacturing Plants: Continuous-Duty Lifting Explained
A production line that stops any time a hoist gets too hot is a fast way to lose money. Plant managers who select lifting gear that is only meant to be used on occasion in the workshop often learn the hard way that it doesn’t cut it once the equipment is in the real manufacturing cycle. Elephant Hoists have a different design brief. They are built for repeated lifts, long shifts, and loads that keep on moving all day long without a break. This guide will help explain what continuous-duty lifting really means, how duty cycle ratings work, and what kind of hoist belongs on a manufacturing floor versus a maintenance bay. Quick Answer: What Counts as Continuous-Duty Lifting A continuous-duty-rated hoist can run for long periods of a shift, start and stop frequently, and carry loads close to its rated capacity without overheating or wearing out prematurely. To summarise, look for: H3, H4, or H5 duty cycle rating per HMI/ASME A motor designed for 25 to 100% running time per hour A brake and gear train for frequent, not occasional, starts Chain or wire rope grades matched to number of daily lift cycles Factory and assembly-line work is covered by electric chain hoist series and manual hoists for lighter, intermittent use. Elephant Hoists cover this range. Why Duty Cycle Rating Matters More Than Lifting Capacity Two hoists can have the same tonnage rating but perform very differently on the factory floor. Capacity tells you how much weight a hoist can lift. The duty cycle tells you how hard and how often it can lift that before something wears out. Industry groups, such as the Hoist Manufacturers Institute (HMI) and the American Society of Mechanical Engineers (ASME), classify hoists based on load spectrum, daily operating time, and frequency of starts. The European Federation of Materials Handling (FEM) and ISO have parallel systems, but each standard has a different name. H1 and H2: Light and Infrequent Use Light and Infrequent Use. Use H1 hoists for suitable powerhouses and utilities and for infrequent handling where loads occasionally approach capacity and the hoist sits idle for long stretches between use. H2 consists of light machine shop work with loads and usage at random throughout the day, with total running time less than 12.5% of the work period. These classes are good for a maintenance bay. They are not the right choice for a manufacturing line that runs a hoist for hours at a time. H3: General Manufacturing and Assembly H3 is for general machine shop fabricating, assembly, storage, and warehousing with randomly distributed loads and utilisation and total running time of less than 25% of the work period. Many mid-volume manufacturing plants are comfortably within this range. H4 and H5: High-Volume and Heavy Service H4 is for heavy loads, generally at rated capacity, and high volume, such as steel warehousing, machine shops, mills, and foundries. Running time up to 50% of the work period. H5 is at the top end for bulk handling, with attachments like buckets or magnets that operate near constantly through a shift. If a plant operates two or three shifts with repeat lifts near rated load, H3 or higher should be specified. Guessing on this rating leads to premature motor burnout, brake wear, and stalled production lines, a pattern lifting equipment specialists say appears when a hoist is specified for the wrong operating intensity rather than the wrong lifting capacity. Elephant Hoist Series Built for Manufacturing Lines Elephant is a Japanese brand of lifting equipment. It is known for its rugged construction and steady load control in tough industrial environments. The electric range has single-phase and three-phase models for the actual running hours that a manufacturing plant needs. Electric chain hoists of the Alpha and Beta series are available in variable- or constant-speed versions with single- and three-phase power supplies. They are matched up with plain, geared or electric trolleys by plants, depending on the distance the load has to go on a monorail or runway beam. SA, FA/FB and DA/DB series step up in capacity and running-time tolerance for heavier, higher-volume applications. These electric hoists with hook suspension are ideal for assembly. lines, packing stations and heavy warehousing where the same lift is repeated hundreds of times a day. Hand-operated C21 and H100 series manual chain hoists are still in use for maintenance work, workshop lifting and light-to-medium tasks where power is unavailable or not required. They are not designed for continuous production cycles, but they are a convenient backup for spot lifts around a plant floor. M.A. Zavery is a full-line elephant supplier, including genuine stock obtained through authorised channels. Its technical team assists manufacturing customers in matching hoist series to actual duty requirements rather than guesswork. Features That Support Continuous-Duty Performance A hoist that is rated for factory floors is different than a light-duty unit in several specific ways: Motor insulation class and duty rating. Continuous-duty motors have insulation rated for continuous heat buildup, not for short bursts. Brakes. A hoist that makes dozens of starts and stops every hour needs a brake designed for that wear pattern, not one designed for infrequent use. Material of gear train. Tempered gears are less susceptible to repeated near-capacity loads than standard-grade components. Chain and hook rating. Galvanised load chains are resistant to wear from repeated cycling and stand up better to plant-floor conditions than untreated chains. Works with trolleys. “Trolleys, either geared or electric, are useful for moving loads along a fixed path, reducing manual effort when transferring loads repetitively. How to Choose the Right Elephant Hoist for Your Plant Here’s a short list of requirements for choosing a hoist for a manufacturing environment: Log your lift cycles each day. Estimate the number of hours the hoist will be operating during peak production. Look at your load %. Determine how close your average lift is to the hoist’s rated capacity. Match the duty class. Manufacturing Lines. Don’t just use H1 or H2 equipment, sold for general workshop
Manual Hoist vs Electric Hoist: How to Choose the Right One
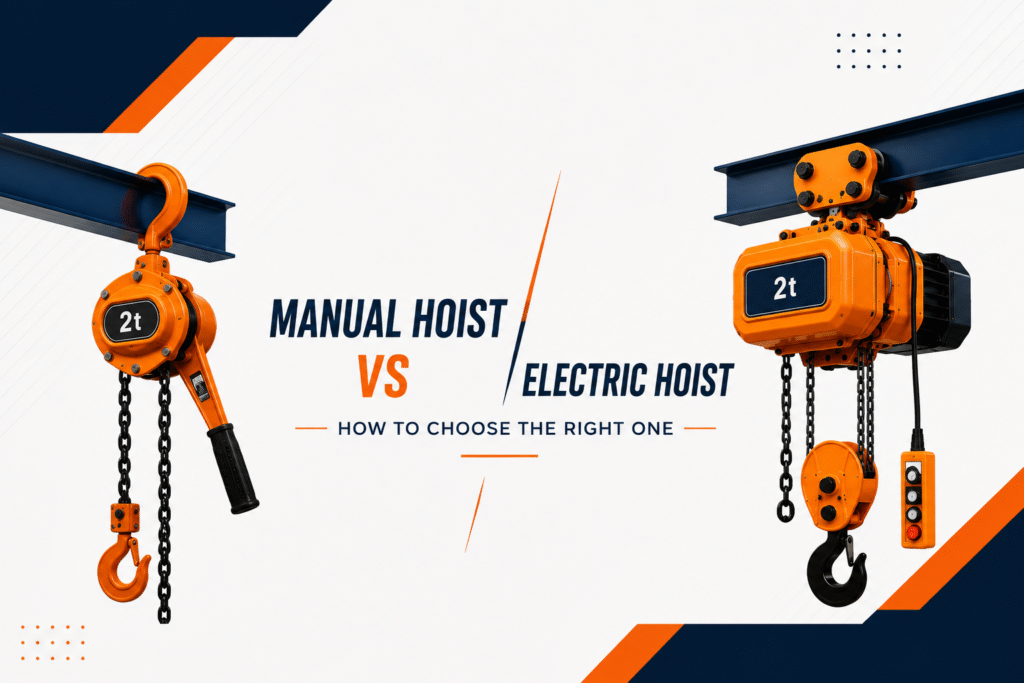
Every lifting job sooner or later comes down to the same question: hand power or motor power? The choice of a manual hoist versus an electric hoist will impact your budget, the speed of your lift, and how often the equipment is used on the floor. Pick the wrong one, and you either overpay for power you rarely use, or you have a hoist that can’t keep pace with your work. This guide describes how each type works, where each one works best, and what to look for before you order. What Is a Manual Hoist? A manual hoist is operated by a man. With a pull on a hand chain or a pump of a lever, gears inside the hoist body multiply your force to lift the load. There are two common forms: Hand chain hoists: a looped chain that you pull, best for straight vertical lifts Lever hoists: useful for lifting, pulling and tensioning at any angle, including sideways or upside down, operated by moving a hand lever back and forth Manual hoists are available with capacities from a few hundred kg to several tonnes from brands such as Elephant (C21 and H100 series chain hoists, YA and Y2 series lever hoists) and Safelift (ratchet lever hoists), so capacity is rarely a limiting factor. The limiting factors for a manual hoist are speed and operator fatigue on repeat lifts. What Is an Electric Hoist? An electric hoist is powered by a motor and is operated with a pendant, push button, or remote. You get a uniform lift speed. You get no operator fatigue. You can lift heavier loads without additional manpower. If you need electric chain hoists for lighter, more frequent lifts in single-phase applications, or for heavier industrial duty in three-phase applications, you can choose from brands such as Elephant (Alpha, Beta, SA, FA/FB and DA/DB series), Yale (CPEF series) and STAHL. Most are equipped with a trolley system, which means the load moves along a beam as well as up and down, making a simple hoist part of a complete material handling system. Manual Hoist vs Electric Hoist: Key Differences Here is a side-by-side comparison of how the two stack up on the points that matter most in making a buying decision. 1. Speed and Output A manual hoist will lift as fast as the operator can pull on the chain or work the lever. Regardless of who is running an electric hoist, it hoists at a constant, steady speed. An electric hoist saves real labour hours over a shift if your team runs the same lift dozens of times a day. 2. Power Supply Manual hoists do not need any electricity at all. This makes them the only realistic choice for remote sites, outdoor jobs where there is no power point, or hazardous areas where powered equipment adds risk. Electric hoists need a stable power supply, either single or three-phase, so you should think about the wiring and load capacity of the site before you buy one. 3. Cost Manual hoists are cheaper to purchase and require less maintenance, as there is no motor, gearbox or control panel to service. Electric hoists are more expensive to buy and install but pay for themselves in labour savings on high-frequency jobs. 4. Load Capacity and Duty Cycle These types are available in a wide range of capacities, from a few hundred kilograms to well over 10 tonnes on heavy-duty electric models. The real difference is the duty cycle. A manual hoist is suitable for occasional or maintenance lifts. Electric hoists are best for continuous or high-frequency lifting where the motor is designed to run repeatedly without overheating. 5. Portability Manual hoists are lighter and easier to move from job to job or workstation. Electric hoists are usually attached to a beam, monorail, or crane system, so they are meant for a permanent lifting point, not a hoist you move around from place to place. Which One Is Right for Your Application? Which One Fits Your Application? How many times will the hoist cycle each day? Many lifts are better. Electric prefers dozens of repeat lifts. Is there power at the lift point? Without a power source, your only real option is the manual. How much does the load weigh, and how far does it move? Heavier, longer travel work generally works better with an electric hoist and trolley. Who runs it and for how long? Pulling it manually can easily lead to a lot of physical strain over a full shift. What is your budget for installation and maintenance? Manual hoists are easier and cheaper to maintain over time, while electric hoists need periodic checks of the motor, brake and control. It’s normal if your answers point in different directions for different parts of your business. Many facilities use both: manual hoists for maintenance bays and occasional lifts, and electric hoists for the production line or high-traffic lifting points. Maintenance Needs for Each Type Manual hoists have no electrical system that can fail but require regular scheduled chain inspection, brake checks, and lubrication. Electric hoists add motor windings, brake discs, limit switches, and control wiring to the list of things to check, so maintenance takes a little longer, but there is far less physical effort required during use. Whatever type you run, keep genuine spare parts in stock and have a regular inspection schedule so the hoist remains within its rated safe working load. Where to Buy Manual and Electric Hoists in India M.A. Zavery & Co. of Kolkata has been supplying lifting equipment to industries across India since 1983. The company has manual hoists from brands Elephant (C21, H100, YA and Y2 series) and Safelift (ratchet lever hoists) and electric chain hoists from brands Elephant (Alpha, Beta, SA, FA/FB and DA/DB series), Yale (CPEF series) and STAHL. Because M.A.Zavery stocks both manual and electric ranges, the team can walk you through the manual hoist vs electric hoist choice based on your real site conditions, load